Nine Cylinder-Head Truths That Debunk the Average Rebuild Advice
The most powerful production six-cylinder is a Porsche flat-six, not a V6—and before you touch a gasket, strip the head completely or risk catastrophic wear. Cast iron and aluminum demand opposite cleaning strategies, degreasers need six to eight hours, and pressure washing is non-negotiable. Flash-rust appears in minutes; hairline cracks hide until you look.
The Most Powerful Production Six-Cylinder Is a Porsche Flat-Six, Not a V6
Porsche's 2018 911 GT2 RS holds the record for the most powerful six-cylinder engine ever fitted to a production car. Its twin-turbocharged 3.8-liter flat-six produces 690 hp and 553 lb-ft of torque, figures that eclipse the Ford GT's 660-hp EcoBoost V6. Porsche achieved the jump over the Turbo S's 580 hp by enlisting its motorsport engineers, who fitted new turbos delivering 22.5 psi of boost, lowered the compression ratio from 9.5:1 to 9.0:1, and raised the rev limit to 7,200 rpm. A longer, smaller-diameter intake manifold kept the air/fuel mixture cooler, while a water-spray system on the intercoolers engages at intake temperatures above 122°F with the throttle at least 90% open, dropping temperatures by 20°F. This allows the engine to sustain maximum power on a racetrack without overheating.
- Power690 hp
- Turbo Boost22.5 psi
- Rev Limit7,200 rpm
- Compression Ratio9.0:1
Before Cleaning a Cylinder Head, Strip It Completely or Risk Catastrophic Wear
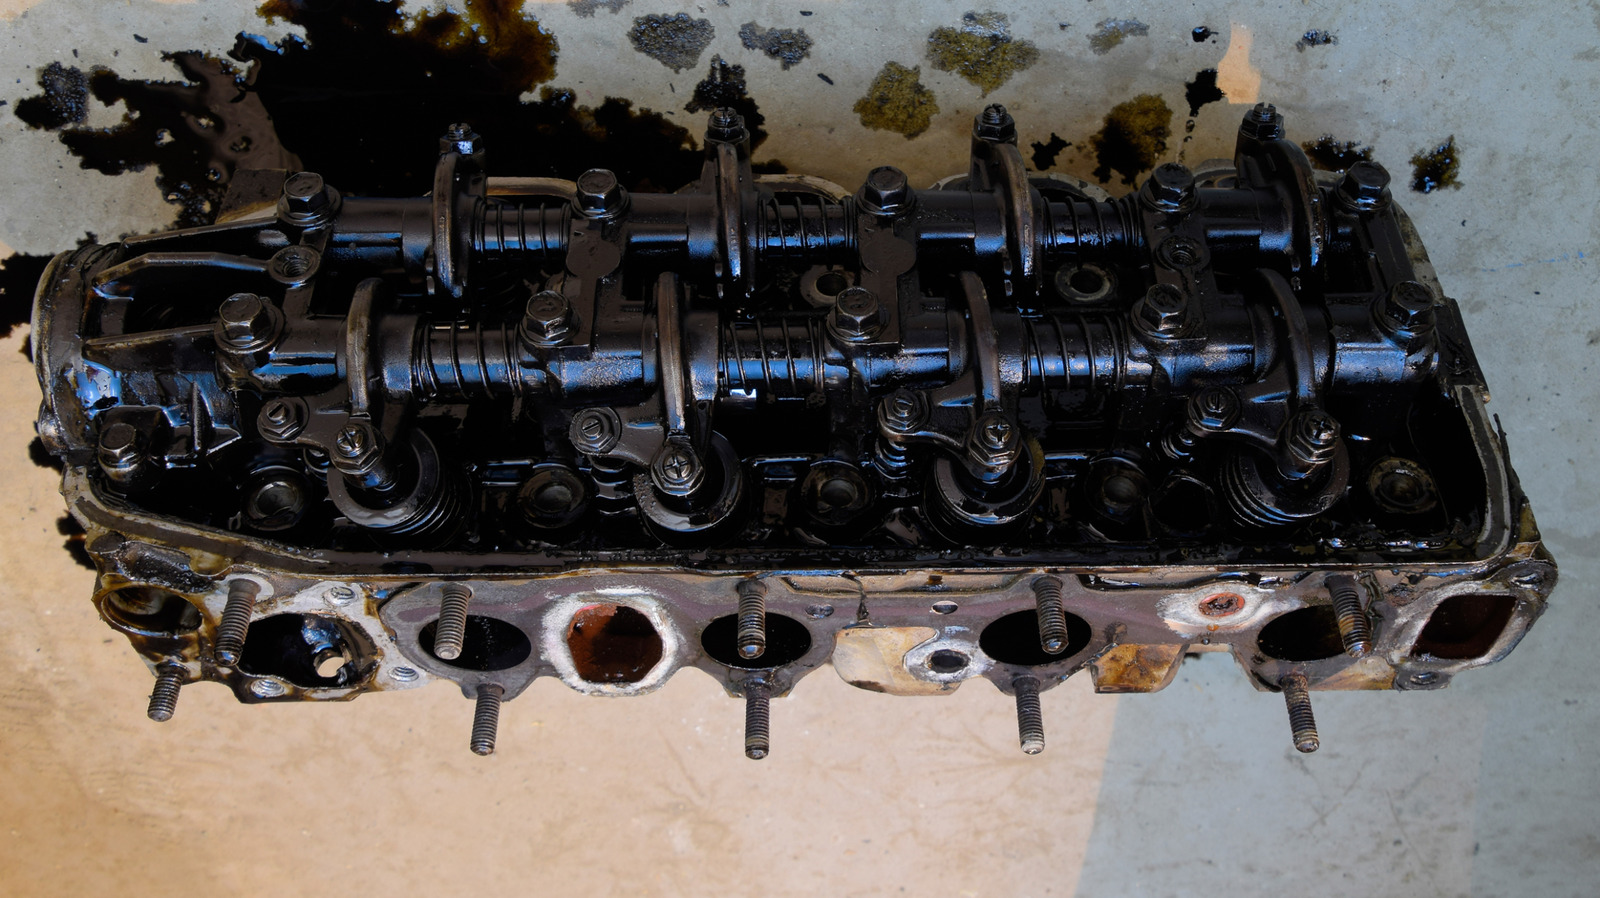
A fully assembled cylinder head is a trap for contamination. When valves, springs, retainers, and valve stem seals remain in place, dirty water and corrosive grit lodge in the valve guides and oil passages. During engine operation, that debris acts like sandpaper on moving parts, accelerating wear until the valve no longer seats properly. To avoid this, use a dedicated valve spring compressor to compress each spring, then remove the springs and valves one by one. Lay out every component on an old egg carton or a labeled cardboard box, mapping each valve to its cylinder. A valve that goes back into a different guide may not seal correctly because each valve has worn a unique pattern over thousands of miles. Once the head is stripped to bare casting, you can also see the metal type and choose the appropriate cleaning chemicals and tools.
- Power660 hp
- Torque550 lb-ft
- Compression Ratio9.0:1
- Displacement3.5 liters
Know Your Metal: Cast Iron and Aluminum Require Opposite Cleaning Strategies
The metal of your cylinder head determines how aggressive you can be. Vintage cast iron is rugged and forgiving — it shrugs off steel scrapers, heavy chemical cleaners, and forceful scraping. Modern aluminum is soft and sensitive: a steel blade can gouge the deck surface, and strong alkaline or caustic cleaners can etch the alloy into a pitted mess. Before reaching for any tool, examine the casting to confirm the material. For aluminum, switch to a plastic gasket scraper and a cleaning-soaked scuff pad, working carefully across the mating surface to lift old gasket material without digging in. Inside exhaust ports, use a brass wire brush to break up carbon crust without damaging the metal. Selecting the wrong tool for the metal can ruin the flat sealing surface, leading to head gasket failure and pre-ignition once the engine is back in service.
- ToolsValve spring compressor
- OrganizationEgg carton method
Plastic Scrapers and Brass Brushes Protect Aluminum Heads During Carbon Removal
Aluminum cylinder heads are soft enough that a steel scraper can leave permanent grooves in the deck surface, which then cannot seal against the head gasket. Instead, use a plastic gasket scraper and hold it perfectly flat to lift petrified gasket fragments without gouging. For the rock-hard carbon crust that lines exhaust ports, a brass wire brush is the right tool — its bristles are softer than aluminum, so they break up carbon in recesses without cutting into the metal. Work slowly, letting the brush do the job rather than forcing it. Steel razor blades are off-limits; even a single slip can score the surface. After scraping, a scuff pad soaked in cleaner can buff away residue without abrasion damage. The goal is to remove all buildup while keeping the mating face flat and smooth, so the new head gasket has a perfect surface to seal against.
- MaterialCast iron
- MaterialAluminum
Heavy-Duty Degreasers Need Six to Eight Hours to Penetrate Baked-On Varnish
After removing the thick carbon chunks by hand, the chemical wash handles the oily varnish that has baked into the metal over decades. Choose a dedicated heavy-duty engine degreaser — for aluminum heads, select a formula labeled safe for aluminum to avoid caustic damage. Spray the entire casting, or use brake cleaner straight from the can. The chemicals must soak for six to eight hours; this dwell time lets the solvent penetrate the varnished oil channels and oil return galleys, loosening deposits that a brush alone cannot reach. After the soak, take a stiff nylon detail brush or an old toothbrush and scrub every intake runner, coolant passage, and corner until the grease turns into a fluid sludge. Skipping the soak means the cleaner only wets the surface, leaving hardened varnish deep inside the oil passages where it can later clog lubrication.
- ToolsPlastic scraper
- ToolsBrass wire brush
- MaterialAluminum
Pressure Washing and Compressed Air Are Non-Negotiable for the Final Rinse
The final rinse removes every trace of degreaser and dislodged grit, because any leftover chemical can contaminate fresh oil or corrode metal later. A pressure washer is ideal — its high-pressure stream reaches into exhaust ports, coolant passages, and bolt holes. If you don't have one, a garden hose with a high-pressure nozzle works nearly as well. Direct the spray through every opening until water runs clear. Immediately after rinsing, use compressed air to blow the head dry, paying special attention to valve guides and threaded holes where water tends to pool. Moisture trapped in those areas can cause corrosion, and when oil is added, it emulsifies with the water, reducing lubrication. Blow out each guide individually until no mist appears. This step is fast but critical — any water left behind becomes a future problem.
- Soak Time6-8 hours
- ChemicalBrake cleaner
Cast Iron Heads Flash-Rust Within Minutes Without Immediate Oil Protection
Bare iron is eager to oxidize: the moment a cast iron head is rinsed and exposed to dry air, a layer of orange flash rust can appear within minutes. That rust flakes off and contaminates the oil system, and it can also create an uneven surface for the head gasket. To stop it, spray the entire casting with a light coat of WD-40 or thin engine oil immediately after blow-drying. The oil forms a barrier that keeps air away from the metal, preserving the clean surface until reassembly. Do this before you set the head aside, even if you plan to reassemble soon. Aluminum heads do not need this treatment, but cast iron owners should treat this step as part of the drying process, not an extra chore. A few seconds of spraying saves hours of later cleaning.
- ToolsPressure washer
- ToolsCompressed air
Inspecting for Hairline Cracks Is the Final Step Before Reassembly
With the head clean and dry, a close visual inspection can reveal damage that was hidden under years of baked-on grime. Look down the valve ports and across the combustion chambers, checking for hairline cracks that may have been masked by carbon deposits. Run your fingers along the machined surfaces to feel for any step or irregularity. A crack in the head can let coolant leak into the cylinder or combustion gases escape, leading to overheating, misfires, and eventual engine failure. If you find a crack, the head is not reusable — it must be replaced, because welding aluminum is rarely successful and iron cracks tend to spread under heat. This is the last opportunity to catch a faulty part before installing the new head gasket and valves. Only when the head passes inspection should you begin reassembly.
- MaterialCast iron
- ProtectionWD-40
Water Spray on Intercoolers: How It Works and Why It Matters
The water-spray system on Porsche's GT2 RS is a targeted response to heat soak: when the intake air temperature climbs to 122°F, the throttle opens at least 90%, and engine speed exceeds 3,000 rpm, a fine mist is injected onto the intercooler cores. The water absorbs heat as it evaporates, dropping intake temperatures by 20°F, which keeps the twin-turbo flat-six producing its rated 690 hp even during sustained track sessions. The spray is triggered repeatedly, not just once, so it maintains the temperature drop over multiple laps. This approach isn't unique to Porsche; Subaru applied a similar system on the Impreza 22B in the late 1990s, and it has since become a recognized method for preserving performance in forced-induction engines. For enthusiasts, retrofitting a water-spray system is a practical way to keep intake temperatures in check during hard driving, especially on turbocharged cars prone to heat soak.
- Trigger122°F intake temp
- Temperature Drop20°F
- RPM Threshold3,000